


 By Revolutionized Team
Revolutionized is reader-supported. When you buy through links on our site, we may earn an affiliate commision. Learn more here.
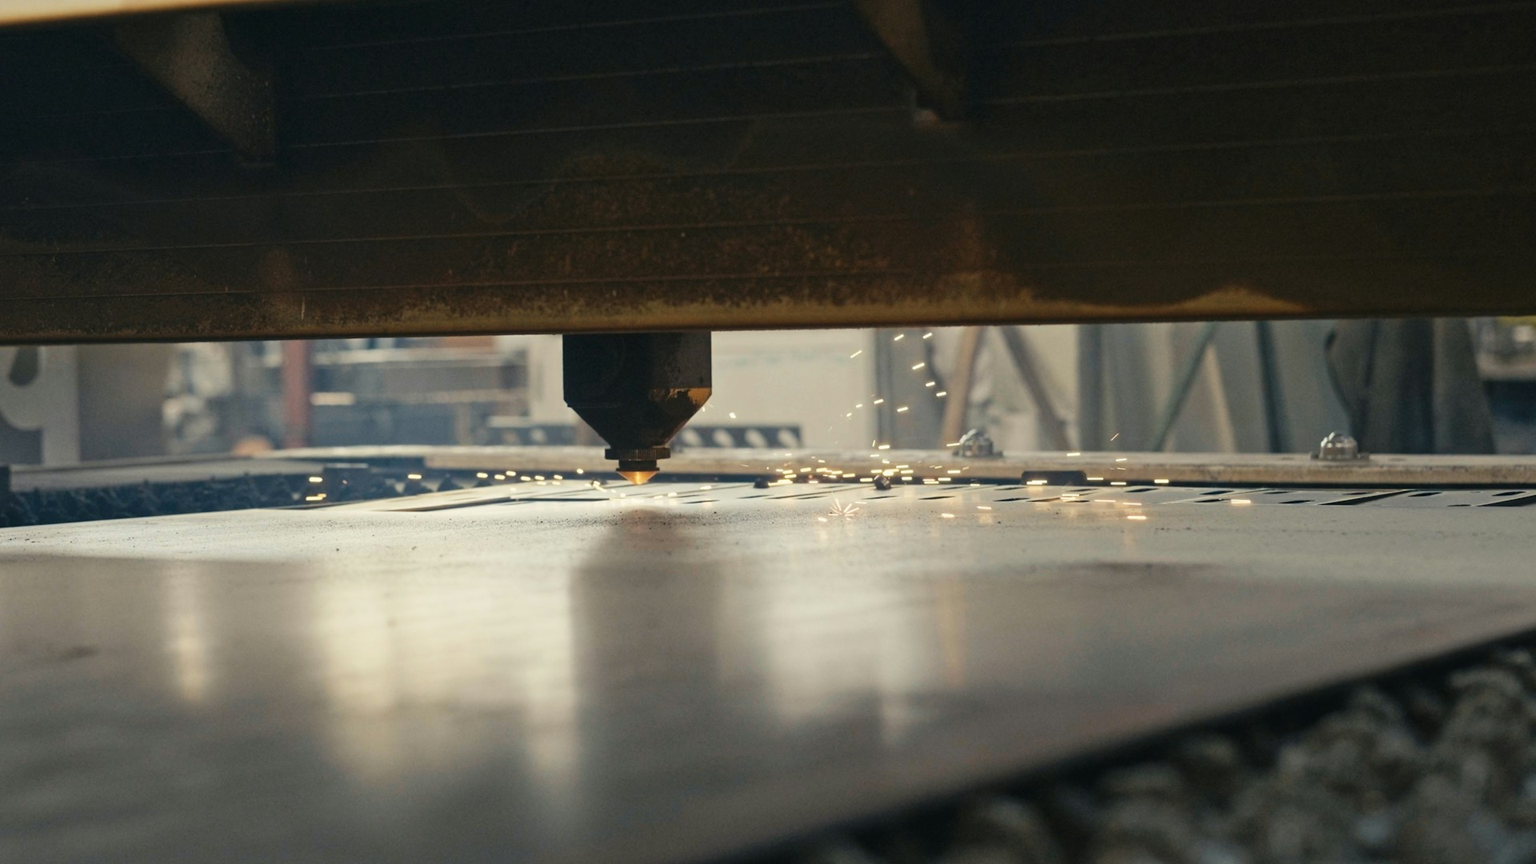
A computer numerical control (CNC) machining center stops mid-cycle when a hydraulic valve sticks, leaving production idle during maintenance. Inspection traces the unexpected halt to debris in the oil that appeared clean.
Choosing hydraulic filters for CNC machines starts with understanding hydraulic cleanliness requirements, since visual checks offer little reassurance. Acceptable limits must reflect the installation’s sensitivity and its manufacturer’s specifications for dependable service.
This guide draws on insights from Chase Filters & Components, a designer and manufacturer of high-pressure filtration systems for industrial manufacturing.
Poor fluid condition can contribute to hydraulic failure before a visible defect points maintenance toward the cause. Troubleshooting should therefore examine both the lubricant and the machine’s hardware. For stationary CNC equipment, connecting a fault with its service history, reviewing manufacturer guidance and checking differential pressure indicators helps avoid assumptions based solely on the first symptom.
A 2023 study examined contamination and declining volumetric efficiency in a hydraulic gear pump and valve, comparing wear particles with medium test dust. The authors note that the dust is harder than typical wear particles, reducing the pump’s volumetric efficiency far more than wear particles did. Those controlled experiments do not establish a breakdown rate for CNC machining centers or predict how long an individual installation will remain in service.
Unplanned downtime includes troubleshooting and the work required to restore reliable operation, while premature wear on valves and actuators adds another maintenance burden. Installing a new component may provide only temporary relief if its underlying cause remains unresolved. Repair planning must also account for the interruption itself, including staffing needs and investigation time before production can resume.
According to Chase Filters & Components, water-related deterioration of lubricants may involve oxidation or reduced protection at metal interfaces. Identifying the physical form of moisture helps distinguish the need for specialized removal from routine particulate control. That distinction should guide treatment discussions, while maintenance teams assess how the operating environment could allow unwanted material into the circuit.
Before choosing a filter, engineers need to identify whether the problem involves debris, moisture or changes to the oil itself.
Debris can enter during assembly or handling, while internal wear generates additional fragments. Particle counting evaluates their concentration and size distribution, helping identify material that threatens close-clearance components even when it is too small for an unaided visual check.
Condensation or seal damage may allow ingress, leaving liquid dissolved, emulsified or separated from the oil. Appearance alone cannot reliably indicate the amount held in solution, so laboratory testing provides a more useful check when maintenance teams suspect moisture exposure. Removal methods include coalescing filtration, vacuum dehydration and centrifugal separation.
Oxidation alters the lubricant’s chemistry, making oil-condition assessment an essential complement to particle counting. Conventional filtration alone does not establish whether the remaining fluid is suitable for continued service or requires replacement.
Equipment specifications identify the cleanliness level required for an installation, while consistent reporting makes results comparable across laboratories. The International Organization for Standardization (ISO) provides that framework through ISO 4406, including a method for coding contamination levels by size. The classification describes measured cleanliness, while equipment-specific guidance defines the applicable acceptance target. Sampling quality also matters when interpreting the result.
The Society of Tribologists and Lubrication Engineers explains the three-number particle count system using cumulative concentrations per milliliter. Its entries classify material at least 4, 6 and 14 microns in size, respectively. Original equipment manufacturer recommendations may distinguish fresh from in-service oil. Higher pressures or tighter tolerances can demand greater fluid purity, making the most contamination-sensitive components relevant when setting acceptance criteria.
Moisture requires its own limit in parts per million because particle-count codes do not specify an allowable dissolved amount. Chase Filters & Components’ experts explain how oil saturation and system requirements influence what an installation can accommodate. Equipment recommendations and lubricant supplier criteria should guide the final acceptance decision. This keeps a general allowance from becoming a substitute for application-specific guidance.
Chase Filters & Components notes that hydraulic and pneumatic filters block damaging contaminants by forcing the system’s fluid or gas to pass through the filter. These contaminants become trapped, preventing them from continuing to circulate and damage the essential components.
Once engineers set cleanliness targets, they can evaluate the assembly’s circuit position and check supplier data against five practical requirements:
Particles can damage closely fitted parts through three-body abrasion and erosion mechanisms, with size relative to moving-surface clearances influencing the outcome.
A filter proposal should explain its selection basis clearly enough for engineers to check before approval. Differences between quoted values and equipment specifications warrant a technical discussion with the supplier.
The most-impactful hydraulic filters for CNC machining centers meet the machine manufacturer’s cleanliness targets at their intended circuit location. Servo or proportional-valve circuits may need pressure-line protection, while return filters require sizing for expected return flow.
Checking viscosity-adjusted pressure-drop curves and peak pressure ratings, then confirming fluid-seal compatibility and the supplier’s basis for efficiency testing is recommended.
Manufacturer guidance and differential pressure indicators should determine replacement timing, since contamination loading varies with operating conditions. When accumulation rises suddenly, recent servicing or fluid-handling activity provides a starting point for investigating possible ingress.
Maintenance records can then show whether routine servicing or an unusual event prompted a change.
Coalescing filtration, vacuum dehydration and centrifugal separation can remove water contamination from hydraulic oil. Laboratory testing offers a clearer check, since appearance alone is not an effective measure of water levels.
Manufacturer specifications provide the reference point for a cleanliness program, while measured oil condition helps maintenance teams decide when to intervene. During inspections or servicing, the team can use those records and filter-selection data to review earlier decisions.
The stalled machining center illustrates the gap between apparently clean oil and verified suitability for continued operation. Hydraulic filters for CNC machines belong within an ongoing condition-control strategy that can help address emerging problems before production stops and maintenance becomes reactive.
Revolutionized is reader-supported. When you buy through links on our site, we may earn an affiliate commision. Learn more here.
This site uses Akismet to reduce spam. Learn how your comment data is processed.